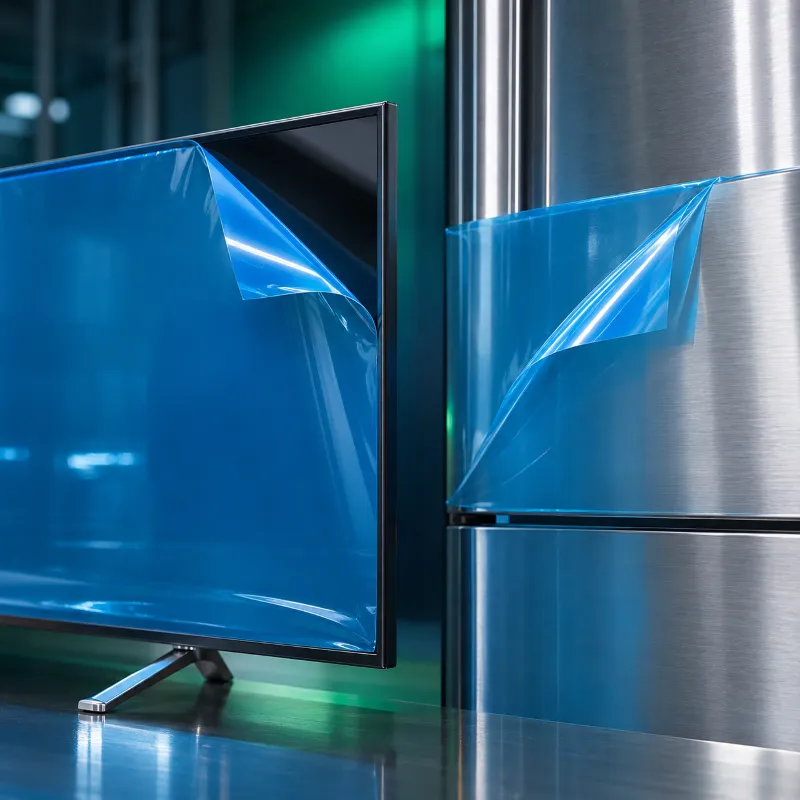
Electronics & Appliance
Protection of panels, glass, metal surfaces, and easy-open packaging for accessories
Know More
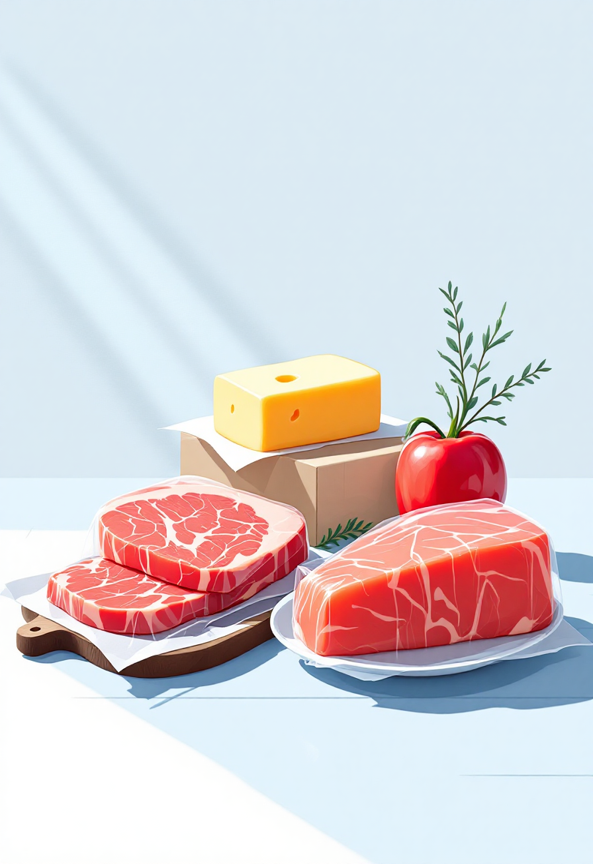
Our Oxygen Barrier Films are advanced multilayer films engineered to deliver maximum protection against oxygen penetration, ensuring superior product freshness, safety, and extended shelf life. Oxygen is one of the primary factors responsible for spoilage, oxidation, and degradation of packaged goods. These films provide an exceptional barrier that keeps oxygen levels under control, making them the ideal choice for industries where product integrity is critical.
Widely used across food & beverage, pharmaceutical, healthcare, agriculture, electronics, and industrial packaging sectors, oxygen barrier films help maintain aroma, flavor, and nutritional value while preventing microbial growth. In agriculture, they are commonly applied as silage covers to preserve fodder, while in electronics and medical packaging, they protect sensitive products from oxidation and environmental stress.
In addition to high barrier performance, these films are designed with excellent mechanical strength, puncture resistance, and sealing compatibility, ensuring reliability during transportation and storage. Available in standard and customizable sizes, they support vacuum packaging, modified atmosphere packaging (MAP), and heat sealing technologies. Eco-friendly and recyclable options are also available, helping businesses achieve sustainability goals without compromising performance.
| Parameter | Specification |
|---|---|
| Oxygen Transmission Rate (OTR) | < 0.1 cm³/m²·24h (23°C, 0% RH) |
| Material Composition | Multilayer (PE / PP) |
| Sealing Compatibility | Heat sealable, vacuum packaging, MAP |
| Clarity | High transparency, printable |
| Durability | High puncture & tear resistance |
| Eco Options | Recyclable / sustainable variants available |
Maintains freshness and prevents spoilage.
Preserves aroma, taste, and nutritional quality.
Withstands puncture and handling stress.
Food, pharma, agriculture, electronics, and industrial use.
Supports branding and product visibility.
Thickness, width, and roll sizes tailored to needs.
Sustainable films for greener packaging solutions.
Protection of panels, glass, metal surfaces, and easy-open packaging for accessories
Know More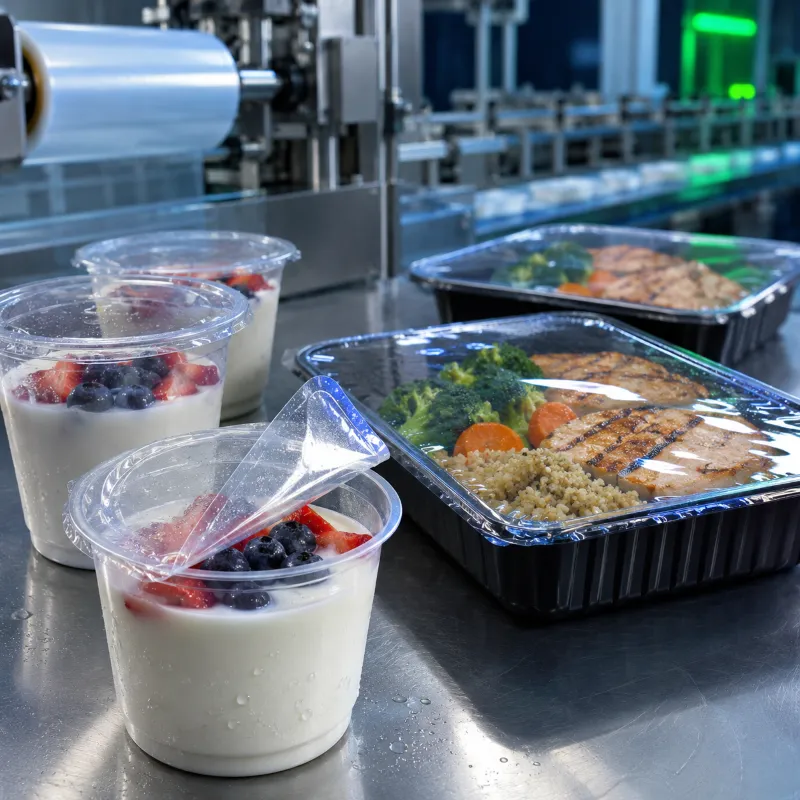
Freshness retention, extended shelf life, convenience packaging (yogurt cups, ready meals)
Know More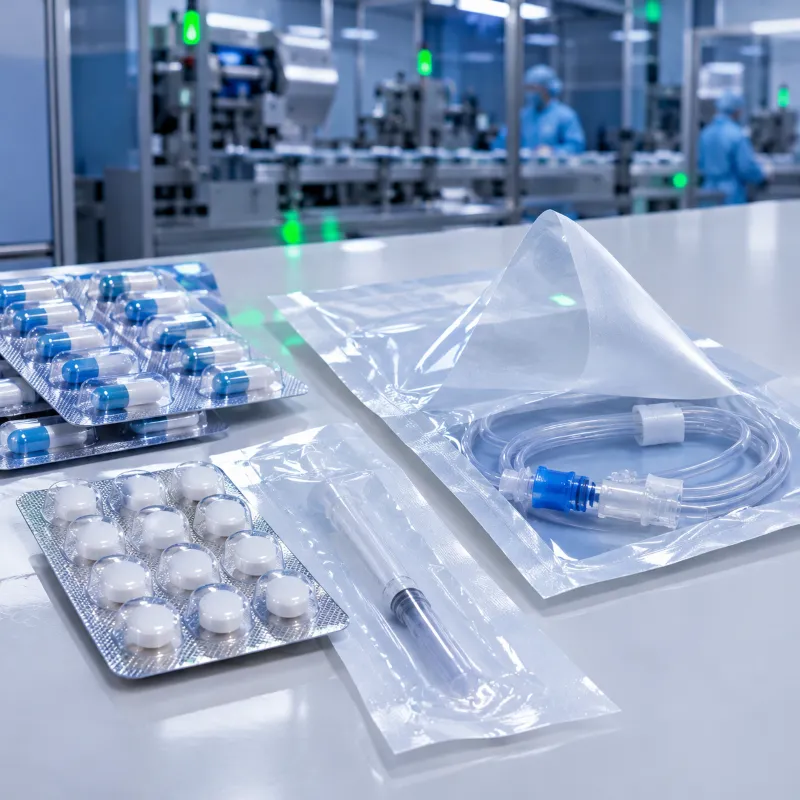
Medical device packaging, blister packs, sterile sealing, easy-open pouches
Know More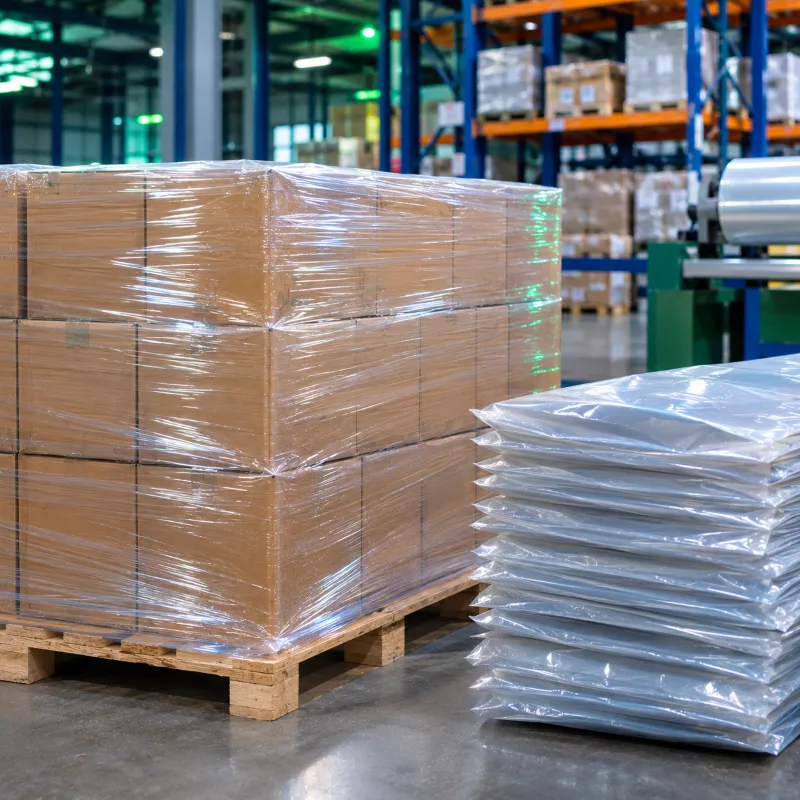
Consumer packaging, carton lamination, pouch sealing, pallet wrapping for logistics
Know More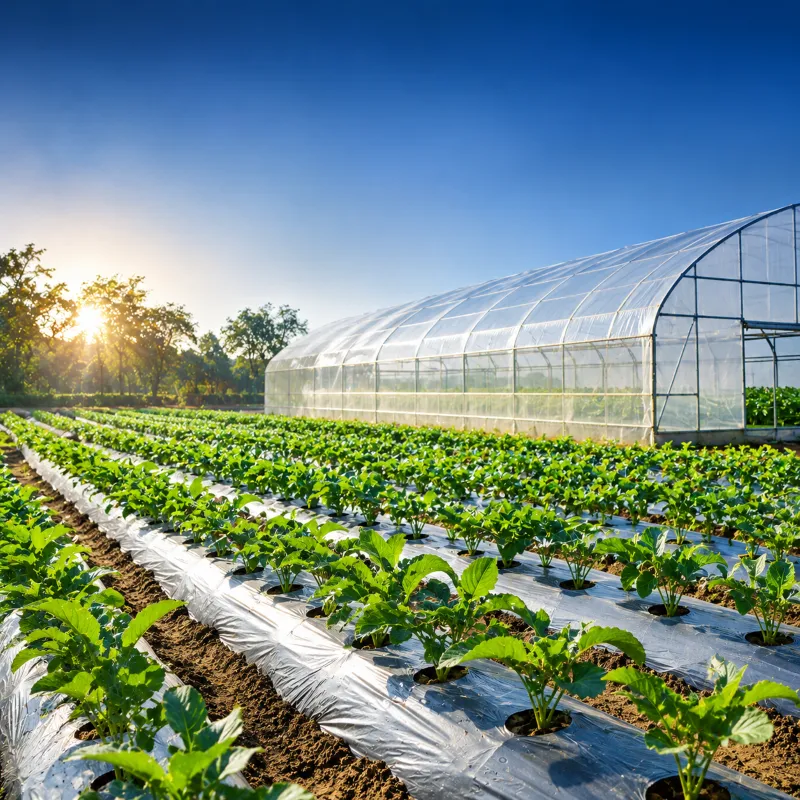
Crop protection, weed control, soil temperature management, greenhouse covering
Know More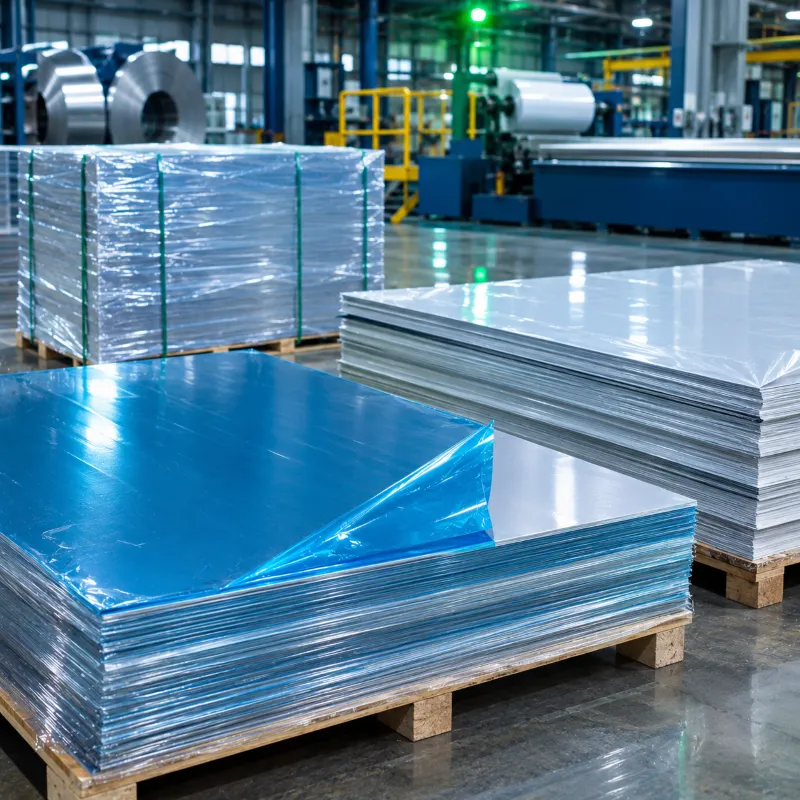
Protection of metal sheets, laminates, composites, palletized shipments
Know More