Key Takeaways
- Oxygen barrier films significantly reduce oxidation, preserving food quality and preventing rancidity.
- Maintaining freshness is crucial; oxygen barrier films limit oxygen transfer for longer-lasting products.
- These films support extended shelf life by minimizing oxygen-related deterioration during storage.
- A professional Moisture Barrier Film Manufacturer can offer combined protection against both moisture and oxygen exposure.
- For aroma-sensitive foods, oxygen control is vital to retain intended flavors and sensory quality.
Ikon Multipack, is a leading manufacturer and exporter of oxygen barrier films.
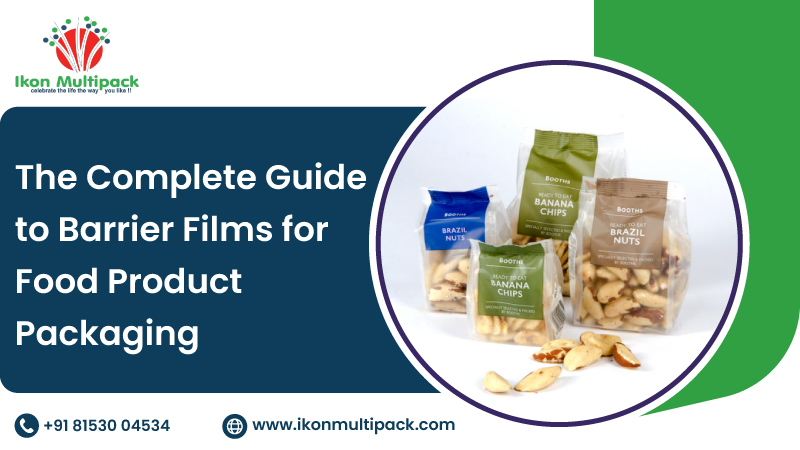
In food packaging, controlling oxygen exposure is important because oxygen can contribute to oxidation, flavour changes and quality deterioration. Oxygen barrier films create a protective layer that limits oxygen transmission, helping packaging maintain product quality throughout storage and distribution.
1. Helps Reduce Oxidation
Oxidation can affect food components such as fats and oils, leading to rancidity, off-flavours and changes in quality. A suitable oxygen barrier film reduces the amount of oxygen reaching the packaged food.
The main benefit is better control of oxygen exposure inside the package. This is particularly useful for products that are sensitive to oxidation.
2. Helps Preserve Freshness
Freshness is a major consideration when selecting packaging for food products. Oxygen entering the package can contribute to deterioration over time, while a well-designed barrier structure limits this transfer.
Our oxygen barrier films can therefore support packaging systems where maintaining the original condition of the food is a key requirement. Barrier performance works alongside the overall package design rather than acting as a standalone preservation method.
3. Supports Longer Shelf Life
Shelf life depends on several factors, including the product itself, storage conditions, packaging structure and oxygen exposure. High oxygen barrier packaging can help reduce oxygen-related deterioration and contribute to longer product stability.
For packaging buyers, this makes oxygen barrier film a practical option when product protection during storage and distribution is a priority. The selected film should match the food product and its specific packaging requirements.
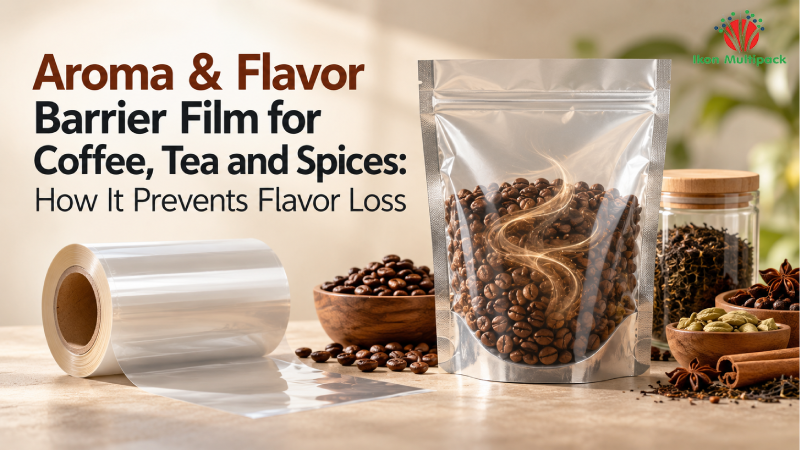
4. Helps Retain Aroma and Flavour
Food quality is not limited to appearance. Aroma and flavour also influence how a product is perceived after packaging and storage.
A suitable barrier structure can help limit the movement of oxygen and other environmental factors that affect sensory quality. For aroma-sensitive foods, oxygen control can be an important part of maintaining the intended product experience.
5. Provides Better Protection During Storage
Food packages may remain in warehouses, distribution centres and retail environments before reaching the consumer. During this period, the packaging needs to act as a protective barrier against external conditions.
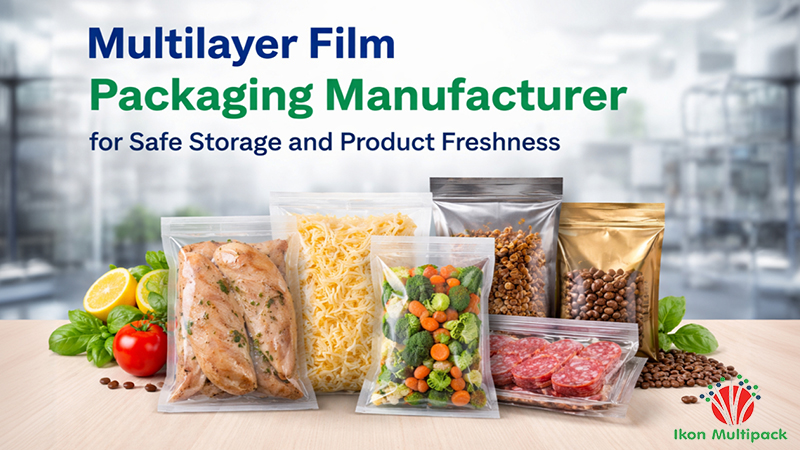
Ikon Multipack develops multilayer barrier film structures intended to control oxygen and moisture permeability for packaged products. Multilayer construction allows different layers to contribute different functional properties within the same film structure.
6. Works With Different Packaging Formats
Oxygen barrier films can be incorporated into flexible packaging structures used for different food applications. Depending on the film construction, packaging systems can support processes such as vacuum packaging, modified atmosphere packaging and heat sealing.
For buyers, the important point is compatibility. The film should be selected according to the filling method, sealing process, product characteristics and expected storage environment.
A Moisture Barrier Film Manufacturer can also help buyers consider oxygen and moisture protection together when both properties matter.
7. Complements Moisture Protection
Oxygen is not the only environmental factor that can affect packaged food. Moisture transmission can also influence texture, freshness and product stability.
That is why barrier packaging is often considered as a combination of properties rather than oxygen protection alone. A suitable Moisture Barrier Film Manufacturer can provide barrier solutions that address moisture exposure alongside other packaging requirements.
When choosing the film structure, buyers should review whether oxygen, moisture, aroma or other barrier properties are most important for the application.
8. Helps Protect Product Quality Through Distribution
Packaging can face mechanical handling, storage movement and changing environmental conditions during distribution. A barrier film needs to provide functional protection while remaining suitable for the intended packaging process.
Our multilayer oxygen barrier films are developed with product protection and packaging performance in mind. The right film structure can help maintain barrier performance while supporting practical packaging operations.
For B2B buyers, evaluating barrier requirements before production can reduce the risk of selecting a film that does not match the application.
9. Supports Multilayer Packaging Design
Multilayer films combine different materials or functional layers to achieve a balance of properties such as barrier performance, sealing and mechanical strength. Oxygen barrier structures may include dedicated barrier materials such as EVOH within a broader film construction.
This approach gives packaging manufacturers more flexibility when developing structures for different food products. A Moisture Barrier Film Manufacturer with multilayer capability can also help address moisture protection where required.
10. Helps Build a More Suitable Packaging System
The final benefit is flexibility in designing packaging around the product. Every food item has different oxygen sensitivity, moisture requirements, processing conditions and storage needs.
Rather than choosing a film based only on the term “high barrier,” buyers should look at the complete application. A good packaging structure balances barrier properties with sealing, handling, processing and product requirements.
A qualified Moisture Barrier Film Manufacturer can be part of this selection process when both oxygen and moisture protection need to be considered.
How to Select the Right Oxygen Barrier Film
Selecting an oxygen barrier film requires more than checking a single specification. Buyers should review the complete packaging application and how the film will perform during production, storage and distribution.
A practical buyer checklist includes:
- Product sensitivity to oxygen and moisture
- Required packaging format and sealing method
- Vacuum or modified atmosphere packaging requirements
- Storage and distribution conditions
- Desired barrier performance
- Mechanical and handling requirements
- Compatibility with the existing packaging line
Discussing these factors with a Moisture Barrier Film Manufacturer can help businesses identify a structure that matches the product rather than selecting a film on barrier performance alone.
Why Choose Us
Ikon Multipack manufactures and exports multilayer barrier films designed for food, pharmaceutical and industrial packaging applications. Our product range includes oxygen barrier, moisture barrier, aroma and flavour barrier, and mineral oil barrier films. We focus on developing film structures that combine barrier protection with practical packaging performance, helping B2B buyers select solutions according to product and process requirements.
Conclusion
Oxygen barrier films play an important role in food packaging because oxygen exposure can contribute to oxidation, flavour deterioration and loss of product quality. By limiting oxygen transmission, the right barrier structure can support freshness, product stability and shelf-life objectives. However, packaging performance depends on more than oxygen protection alone. Moisture, sealing, handling, storage and processing conditions also matter. Choosing the right multilayer structure therefore requires a clear understanding of the food product and its packaging environment. Working with an experienced Moisture Barrier Film Manufacturer can help buyers evaluate these requirements and select a more suitable packaging solution.
Looking for oxygen barrier films for your food packaging application? Contact Ikon Multipack at +91 8153004534 or email info@ikonmultipack.com to discuss your packaging requirements and suitable barrier film options.
Frequently Asked Questions
What are the key benefits of using oxygen barrier films in food packaging?
Oxygen barrier films help reduce oxidation, preserve freshness, support longer shelf life, retain aroma and flavor, and provide better protection during storage. These films limit oxygen transmission, which is crucial for maintaining the quality of food products throughout storage and distribution.
How do moisture barrier films complement oxygen barrier films?
Moisture barrier films work alongside oxygen barrier films to protect food from both oxygen exposure and moisture transmission. This combination ensures the texture, freshness, and overall quality of the packaged product are maintained.
Why should I choose Ikon Multipack as my moisture barrier film manufacturer?
Ikon Multipack specializes in multilayer barrier films designed specifically for food packaging, offering solutions that combine barrier protection with practical packaging performance. Our expertise can help businesses select the right film structure based on product sensitivity, packaging requirements, and storage conditions.
What factors should I consider when selecting an oxygen barrier film?
When selecting an oxygen barrier film, consider product sensitivity to oxygen and moisture, required packaging format, sealing method, and storage conditions. It's essential to evaluate these factors in collaboration with a moisture barrier film manufacturer to ensure optimal performance.
How does an oxygen barrier film affect product shelf life?
An oxygen barrier film can significantly extend a product's shelf life by preventing oxidation-related deterioration. By limiting oxygen exposure, these films help maintain product stability, which is particularly important for perishable items.